CNC Turning Services: Where Round Parts Get Cheap and Precise
If your part is round, it should probably be turned. Bar-fed lathes remove metal faster than any mill, hold roundness a mill can't reach, and run production continuously — which is why a turned shaft routinely prices at half of the same geometry milled. This page covers our turning and mill-turn capability, what the process does best, and the design details that move your quote the most.
What we turn
- Precision turned parts — shafts, pins, spacers, bushings, fittings, nozzles, rollers
- Threaded components — NPT, BSP, metric, UN threads; single and multi-start; acme and trapezoidal
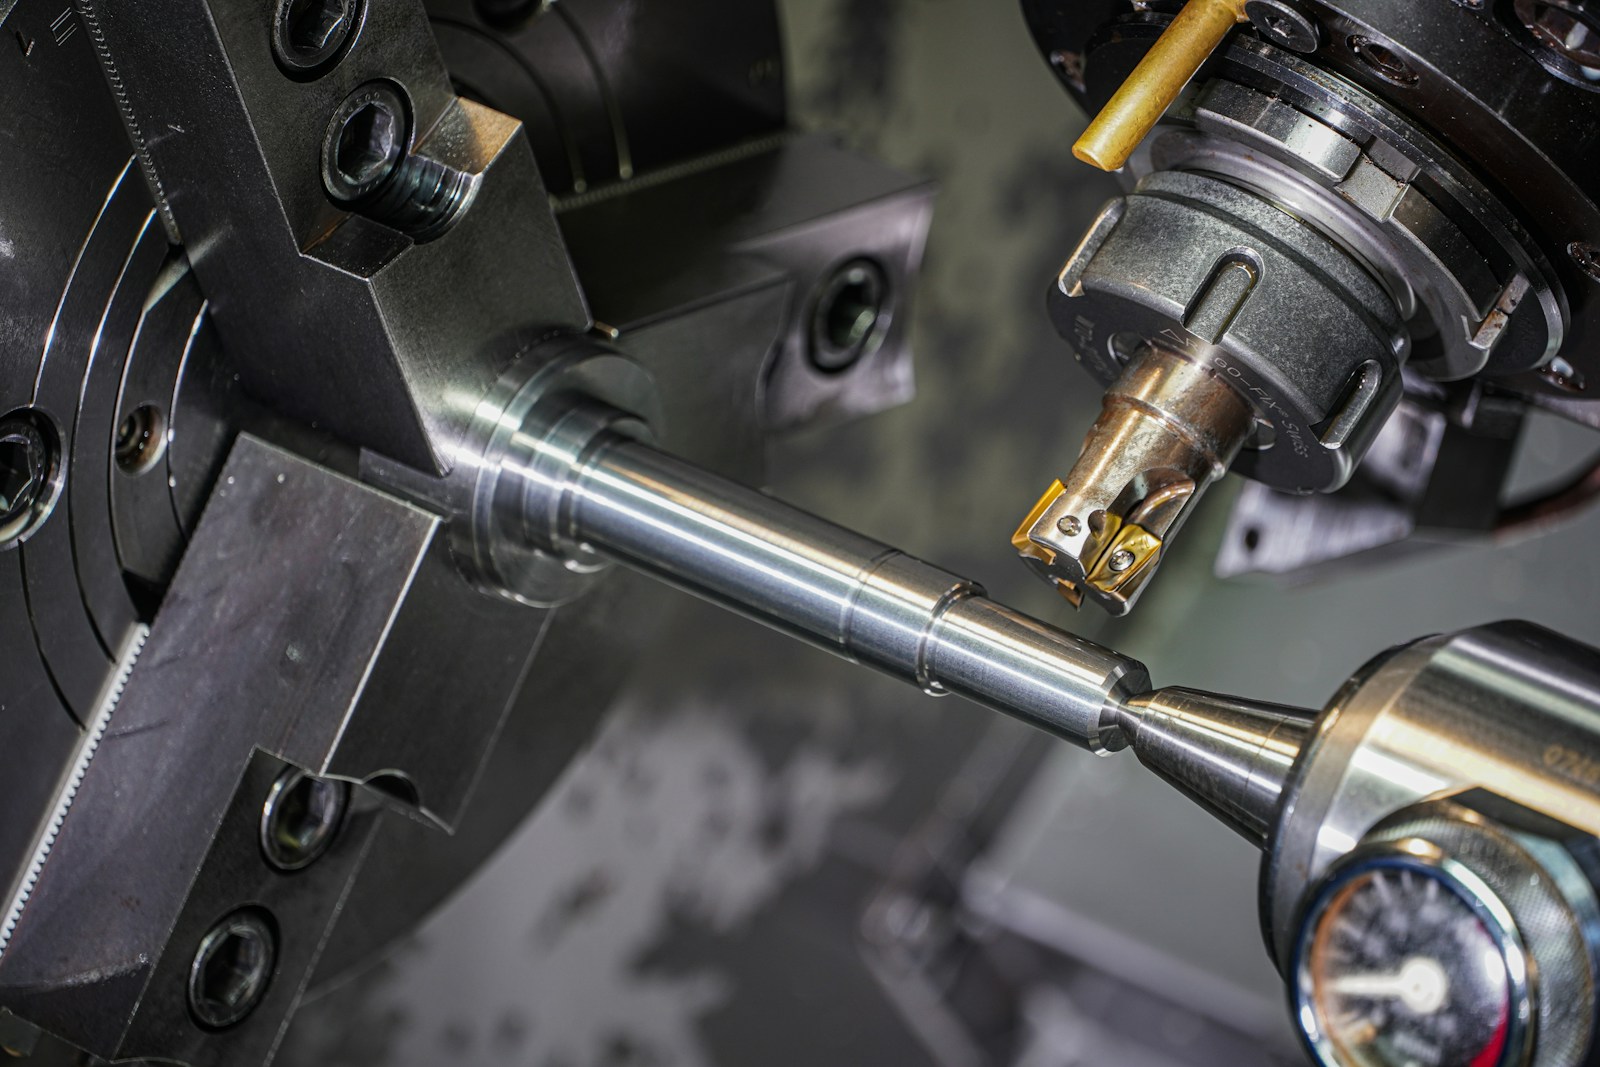
- Mill-turn parts — hex flats, cross-holes, end milled features, slots and keyways in one setup
- Thin-wall and deep-bore work — tubes, sleeves and bores with controlled wall thickness
Capability envelope
| Parameter | Capability |
|---|---|
| Max swing diameter | Ø320 mm |
| Max turning length | 600 mm (bar-fed to Ø32 mm) |
| Standard tolerance | ±0.05 mm |
| Critical diameters | ±0.005 mm, gauge-verified, 100% inspection available |
| Roundness / cylindricity | 0.005 mm on precision work |
| Surface finish | Ra 0.8 µm standard turning; Ra 0.4 µm with fine turning passes |
| Live tooling | Yes — cross-drilling, milling, tapping in-setup |
| Materials | Aluminum, stainless 303/304/316/17-4PH, carbon steel, brass, copper, titanium, PEEK/POM/delrin |
Design notes that lower your turning quote
- Stay round where possible. Every flat, cross-hole or milled pocket on an otherwise round part either needs live tooling or a second op. On bar-fed work, a design that stays 100% turned can cost 30–60% less than one that "mostly" is.
- Relieve internal corners. An undercut groove at a shoulder lets the tool exit cleanly and lets mating parts seat fully — same trick as a drill point relief at the bottom of a blind bore.
- Specify thread classes, not magic numbers. 6g/6H on metric or 2A/2B on inch threads quotes correctly; a tolerance pinned to four decimals on a thread pitch diameter usually means someone measured a good part wrong.
- Tighten only the bearing and seal seats. The rest of a shaft tolerances at ±0.05 mm without consequence — the same rule from our tolerances guide, doubled in value on high-volume turned parts.
- Choose free-machining grades for high volume. 303 stainless or 360 brass machine dramatically faster than 316 or 304 — sometimes the right material choice pays for itself across a production run.
Quality and documentation
Turning is the easiest process to verify — diameters measure directly, quickly and continuously. We offer: air-gauge or micrometer verification on critical diameters, thread go/no-go gauging, surface finish measurement, and full dimensional reports with shipments. For seal and bearing seats we measure roundness, not just diameter — because that's the callout your assembly actually depends on.
Frequently asked questions
What's the minimum quantity for turned parts?
Prototypes welcome — single-piece turning runs daily. Bar-fed economics start working in your favor from ~100 pieces, and dominate from 1,000 up. We'll quote both routes if the crossover is near.
Can you turn parts and anodize or plate them?
Yes — anodizing, black oxide, nickel and chrome plating are coordinated locally, with post-finish dimensions specified and verified where the drawing requires it.
Can you match an existing part without a drawing?
Send the physical sample or a photo with dimensions. We'll reverse-engineer and confirm the critical dimensions with you before quoting — common for legacy and obsolete replacement parts.
Related: 5-axis CNC machining · Full service overview · Rapid prototyping & low-volume production